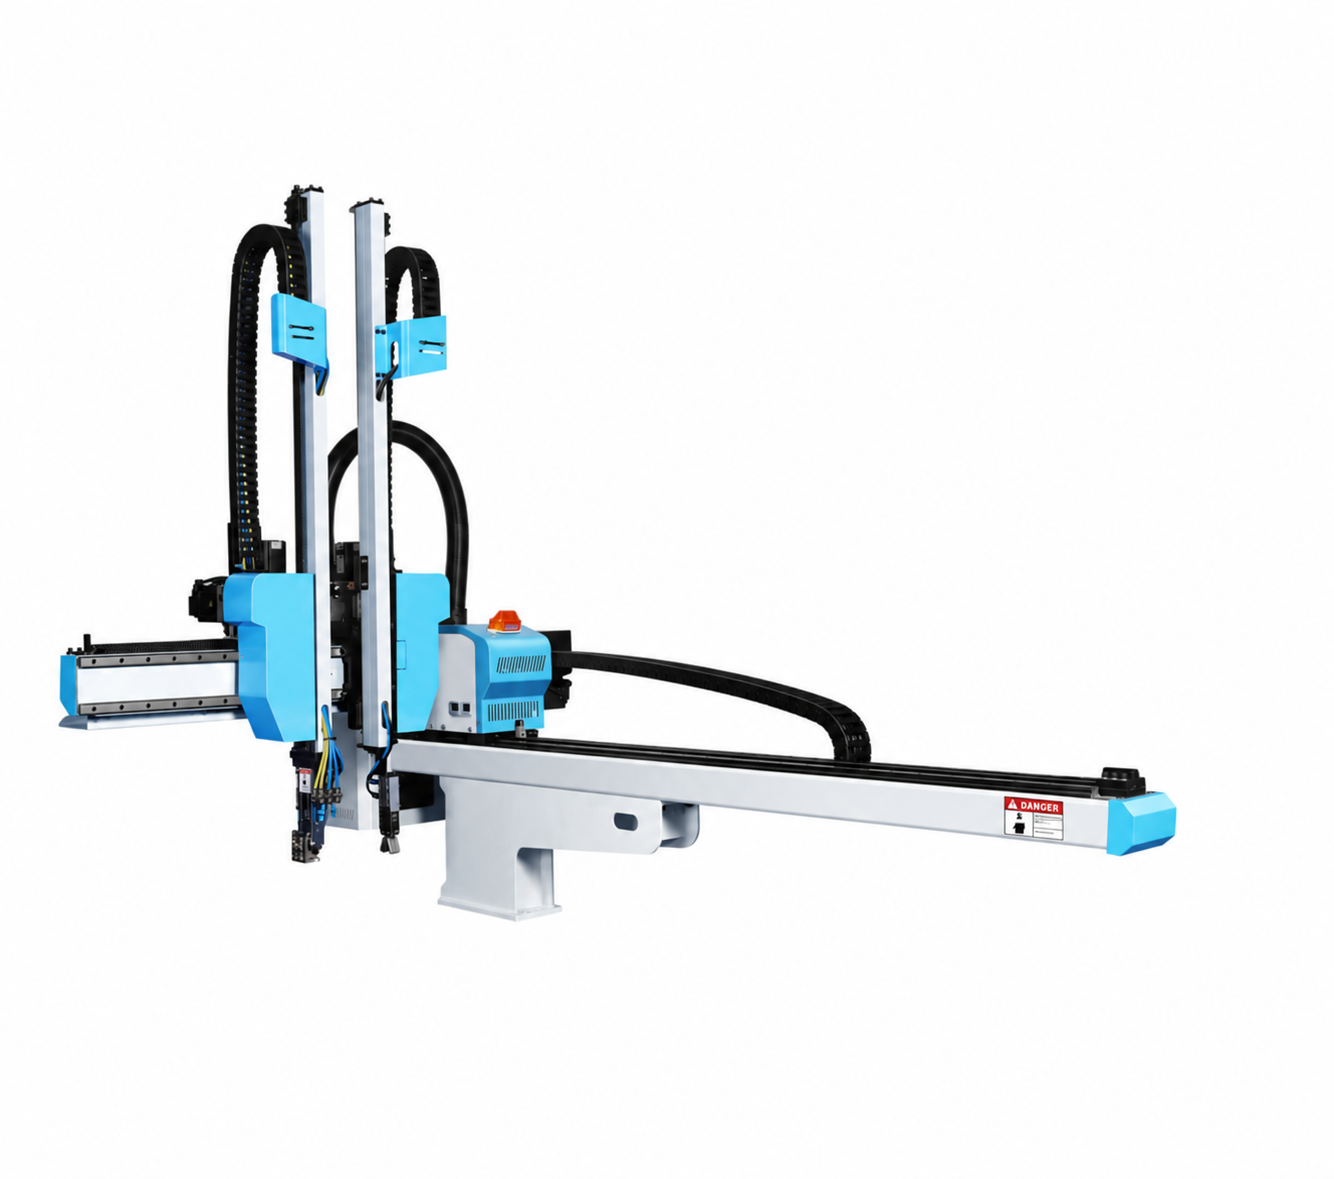
MNS5 / MNSW5-800
CNC full servo injection molding robot
1-stage take-out robot for 50–220-ton horizontal injection molding machines. ±0.1 mm repeatability; compare strokes, payloads and cycle times by model.
Compare 18 CNC full servo robot models for injection molding and vertical press automation. Explore 3-axis and 5-axis take-out robots, 2-axis press robots, single-stage and telescopic arms, 3–80 kg payloads, model specifications and installation drawings.
1-stage take-out robot for 50–220-ton horizontal injection molding machines. ±0.1 mm repeatability; compare strokes, payloads and cycle times by model.
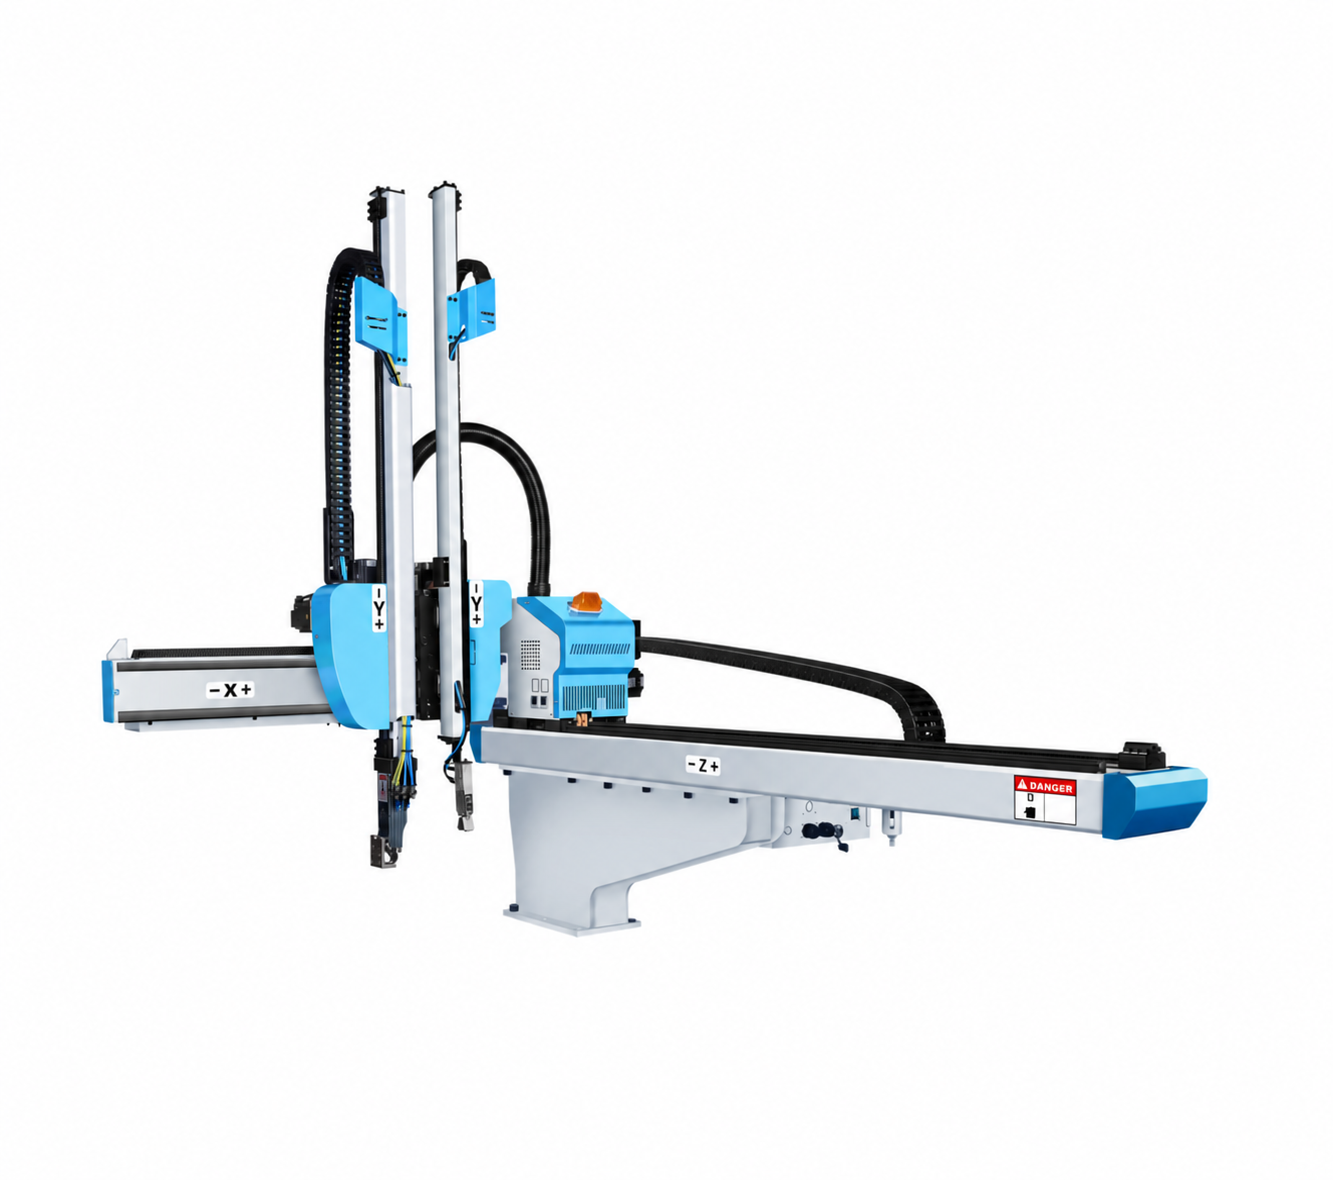
1-stage take-out robot for 120–320-ton horizontal injection molding machines. ±0.1 mm repeatability; compare strokes, payloads and cycle times by model.
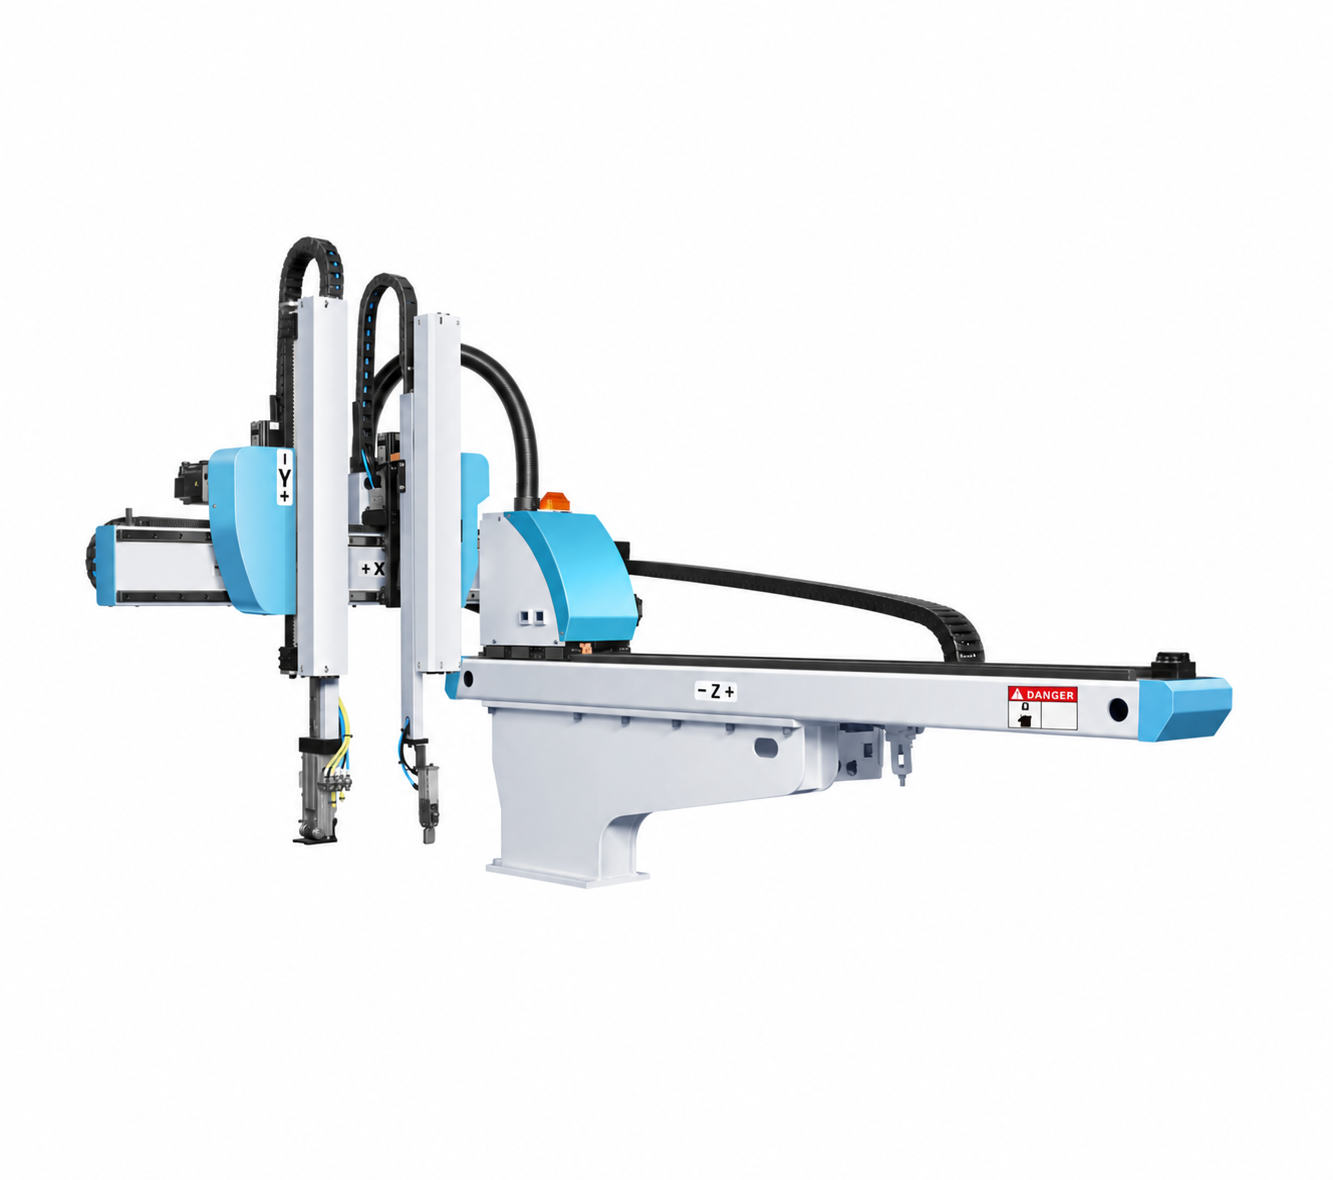
2-stage take-out robot for 200–500-ton horizontal injection molding machines. ±0.1 mm repeatability; compare strokes, payloads and cycle times by model.
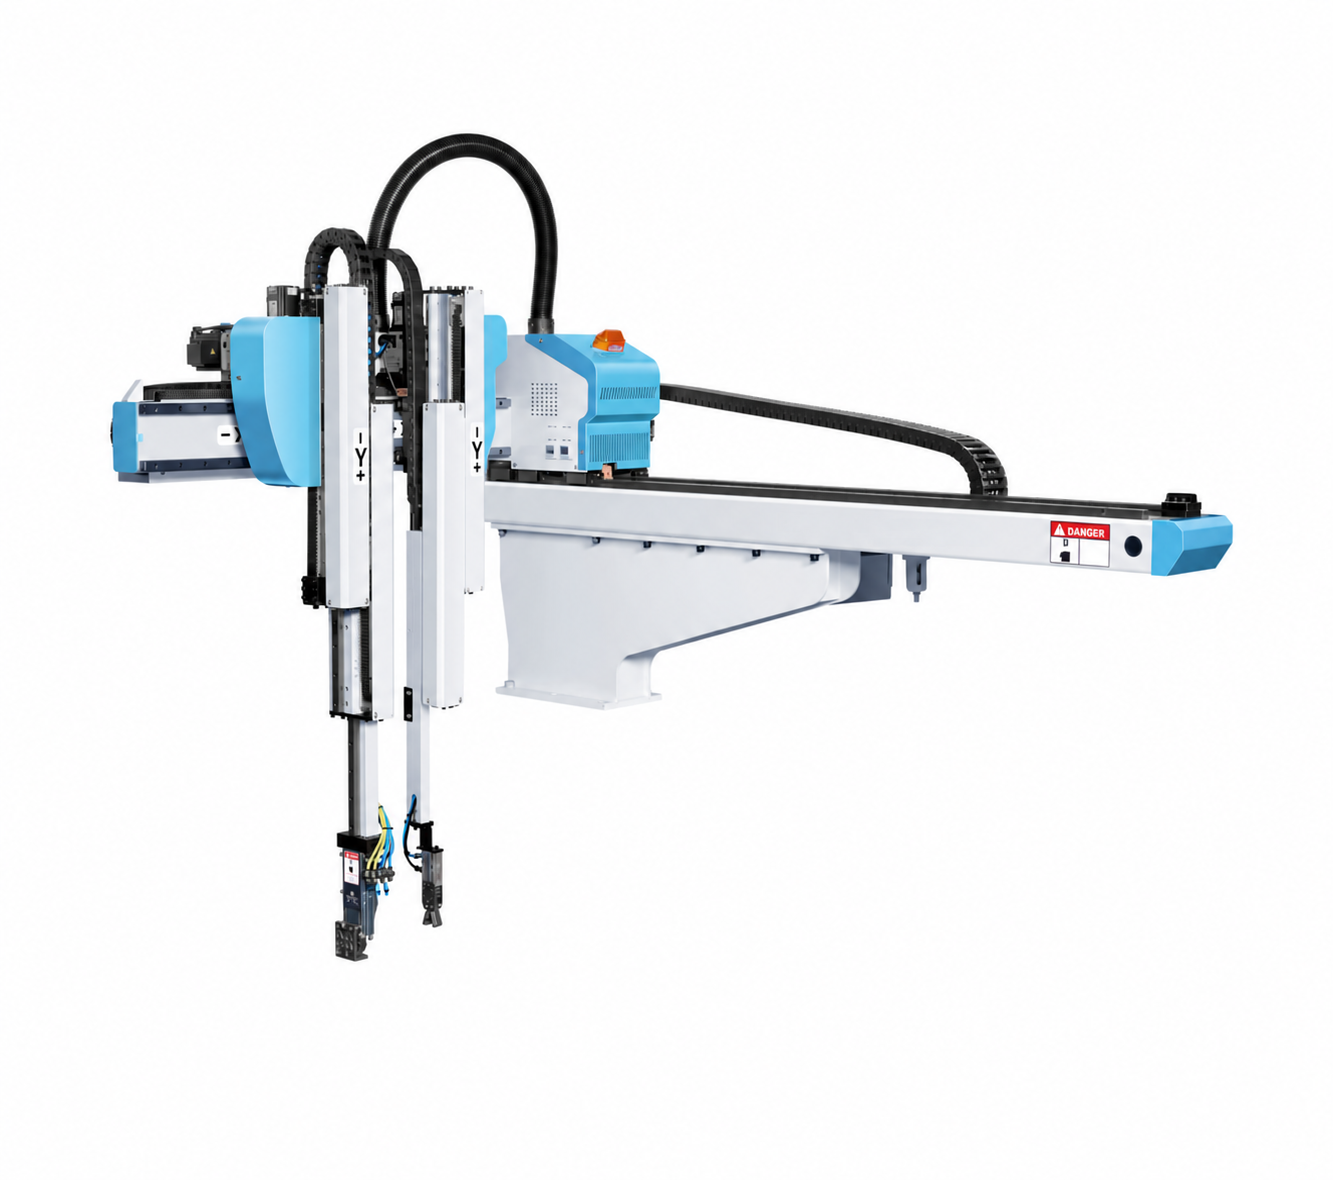
3-stage take-out robot for 120–380-ton horizontal injection molding machines. ±0.1 mm repeatability; compare strokes, payloads and cycle times by model.
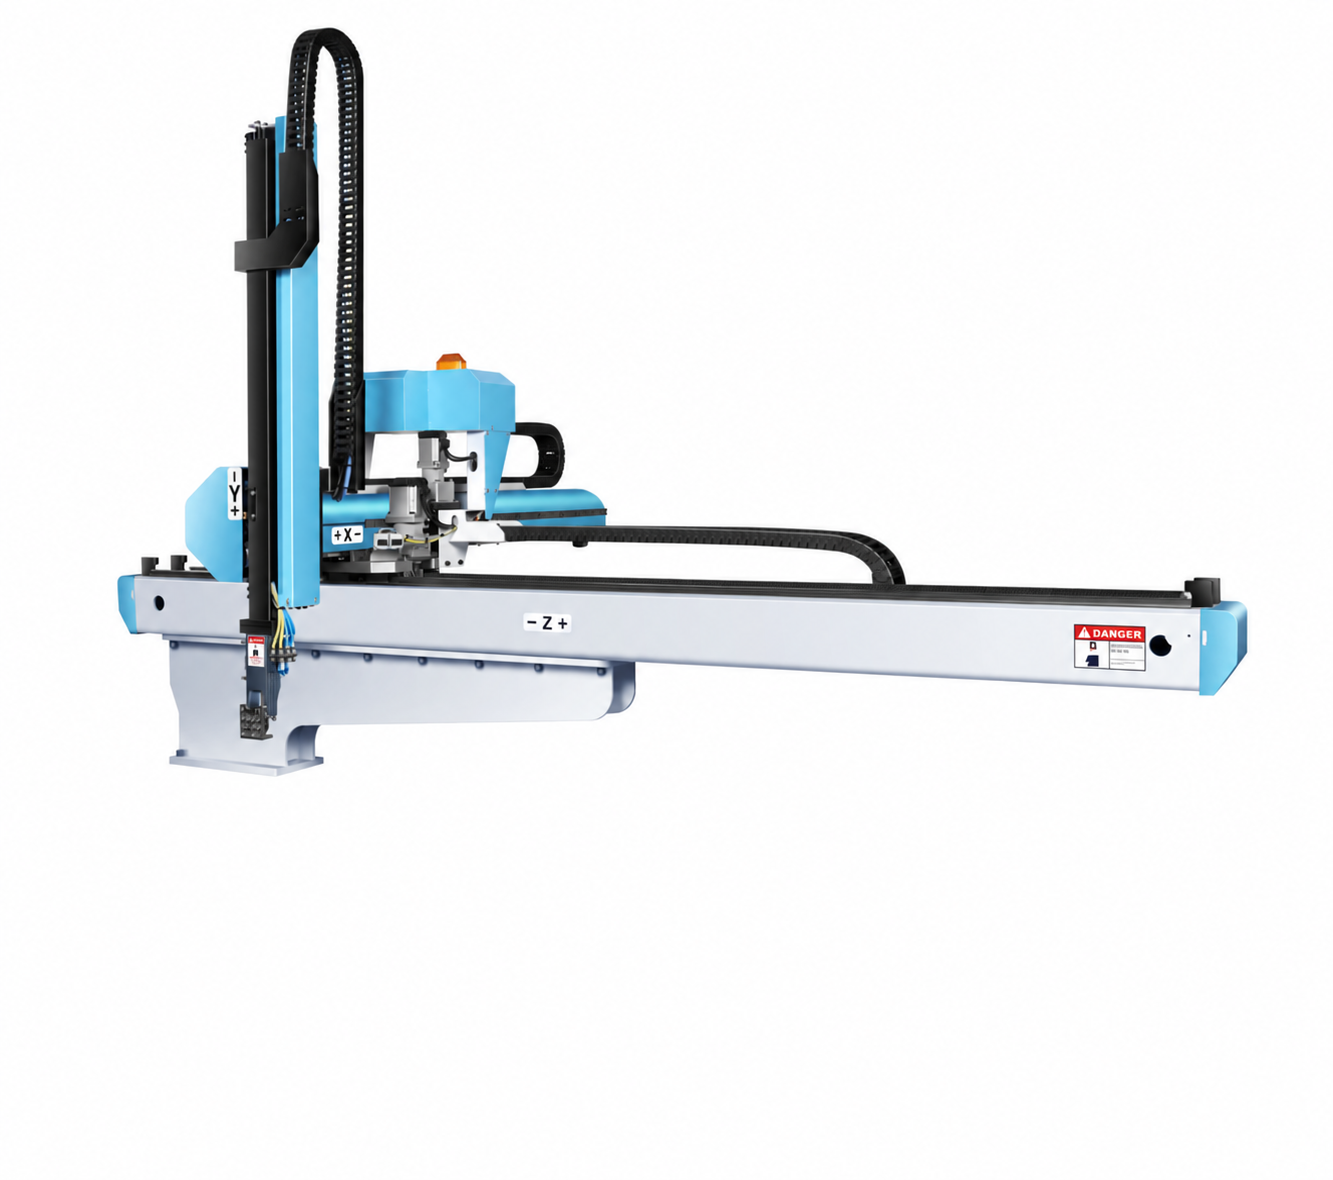
2-stage take-out robot for 200–550-ton horizontal injection molding machines. ±0.1 mm repeatability; compare strokes, payloads and cycle times by model.
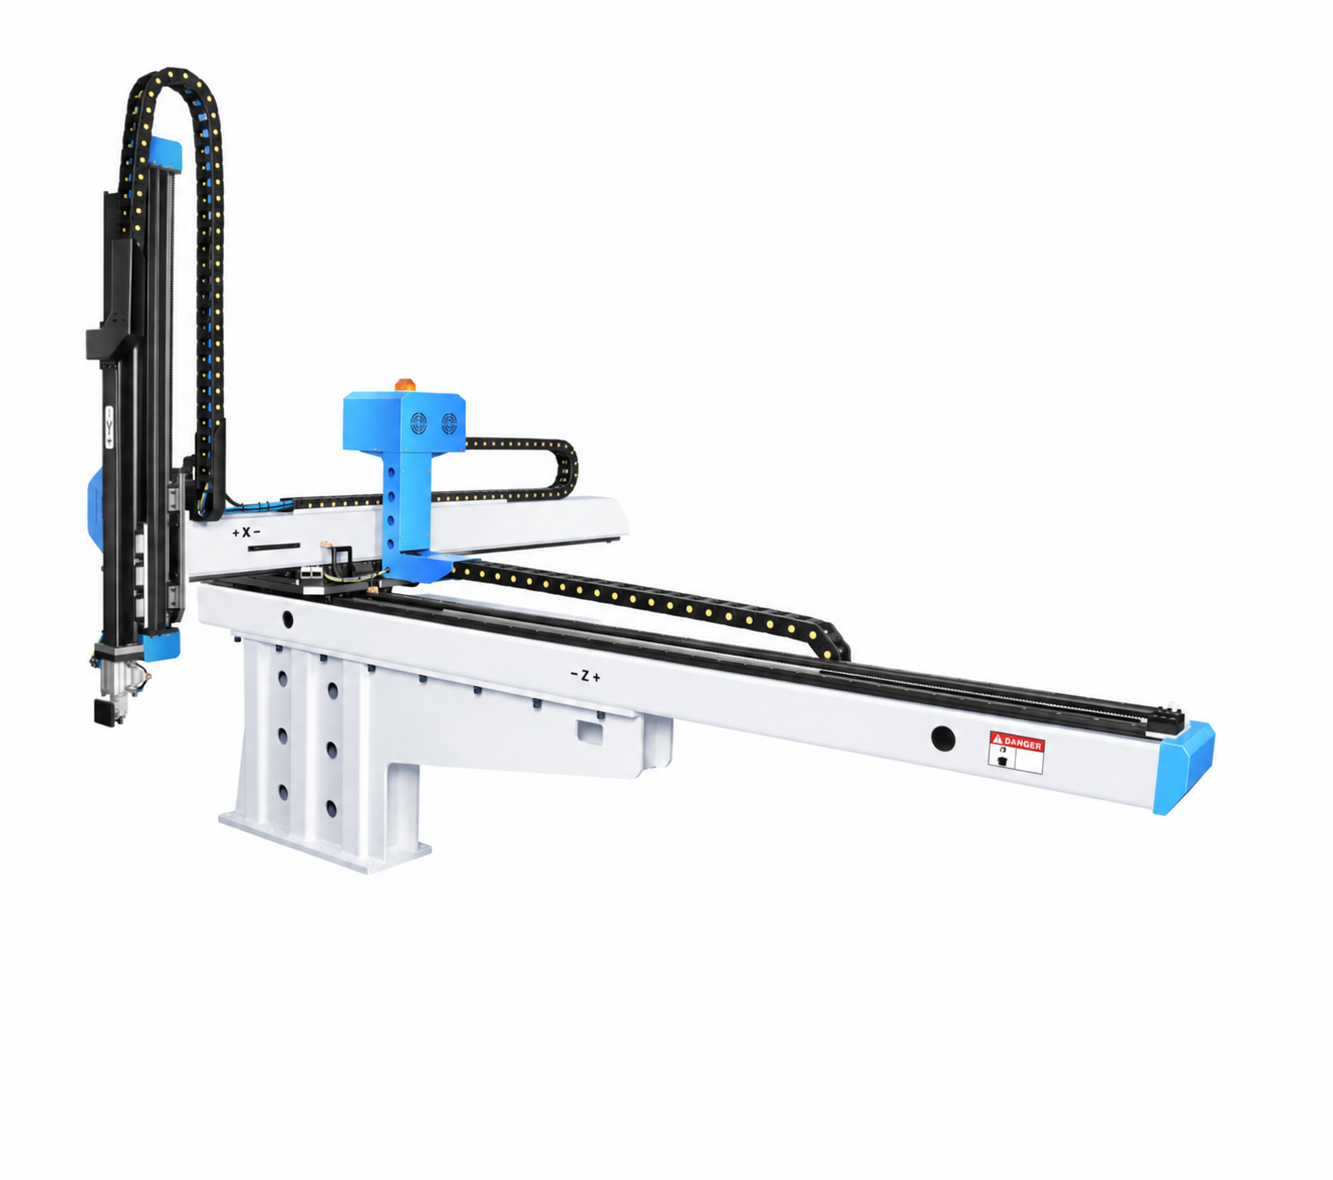
2-stage take-out robot for 450–1500-ton horizontal injection molding machines. ±0.3 mm repeatability; compare strokes, payloads and cycle times by model.
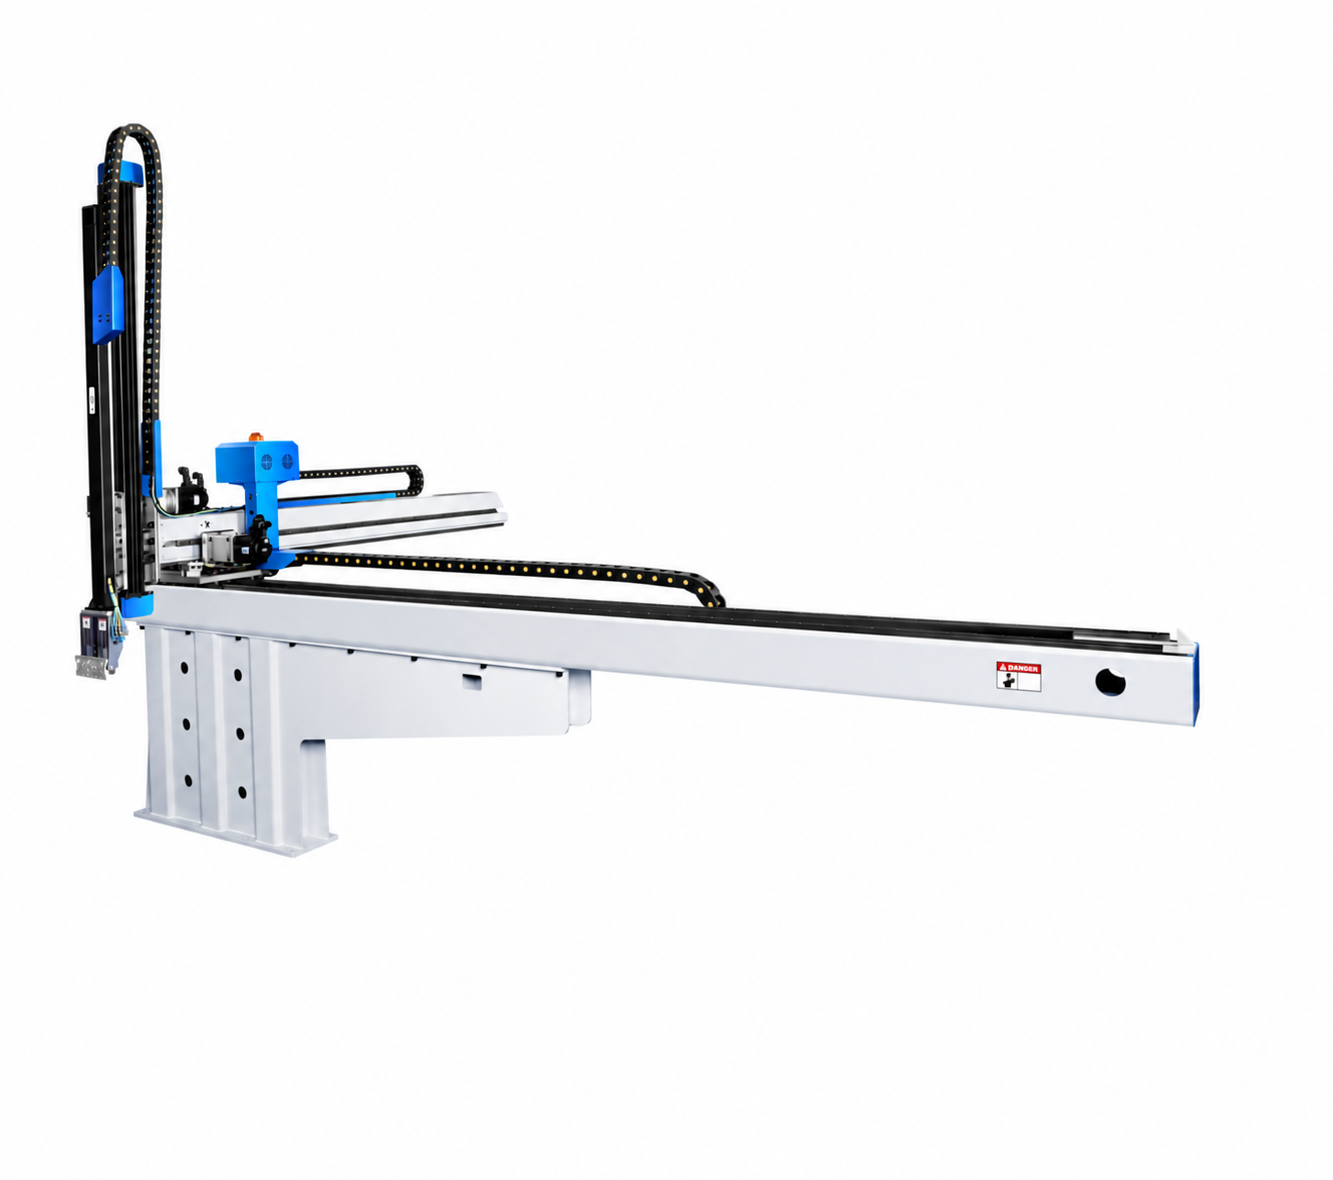
2-stage take-out robot for 1400–3200-ton horizontal injection molding machines. ±0.3 mm repeatability; compare strokes, payloads and cycle times by model.
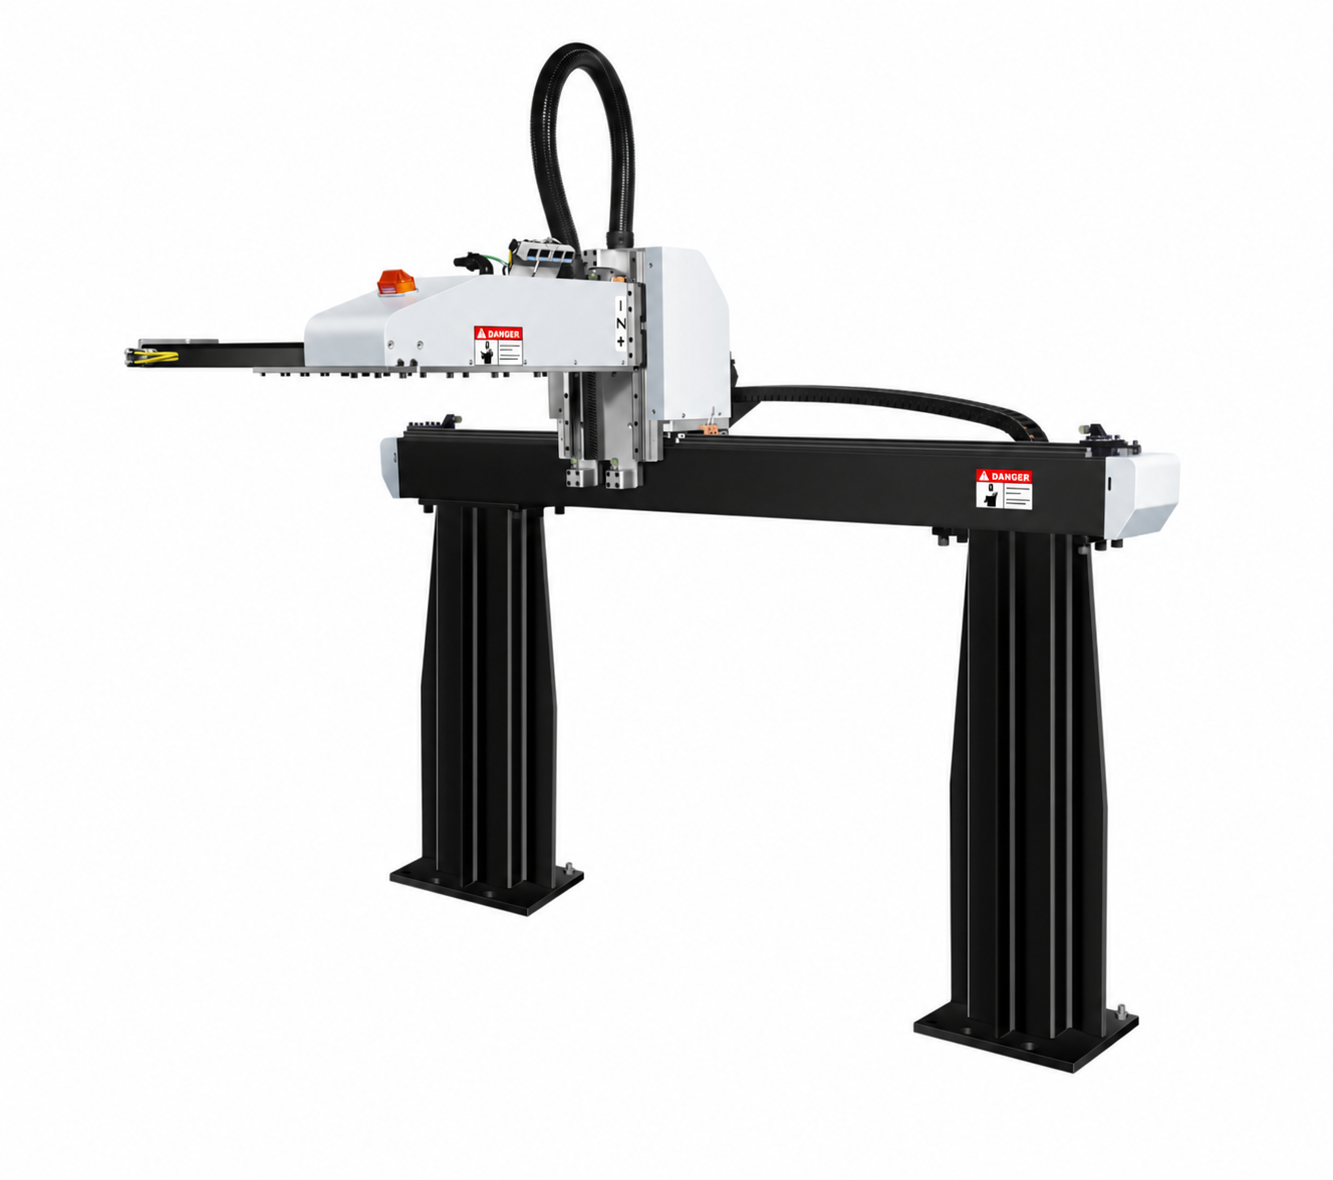
1-stage press handling robot for 50–200-ton vertical thermoforming presses. ±0.1 mm repeatability; compare strokes, payloads and cycle times by model.
| Model | Machine (ton) | Vertical stroke (mm) | Payload (kg) | Take-out (s) | Cycle (s) |
|---|---|---|---|---|---|
| MNS5-800 | 50–220 | 800 | 3 | 0.9 | 10 |
| MNSW5-800 | 50–200 | 800 | 3 | 0.9 | 10 |
| SYS5-800 | 120–220 | 800 | 8 | 1.2 | 12 |
| SYS5-1000 | 120–320 | 1000 | 6 | 1.4 | 14 |
| SW5-1000 | 200–320 | 1000 | 6 | 1.3 | 12 |
| SW5-1200 | 200–500 | 1200 | 5 | 1.6 | 14 |
| S5-3-900 | 120–250 | 900 | 6 | 1 | 10 |
| S5-3-1100 | 160–380 | 1100 | 5 | 1.3 | 11 |
| SYNS3-1000 | 200–320 | 800 | 12 | 1.2 | 10 |
| SYNS3-1200 | 250–380 | 800 | 10 | 1.3 | 12 |
| SYNS3-1400 | 250–550 | 1050 | 8 | 1.3 | 15 |
| SYNS3-1600 | 450–800 | 1600 | 25 | 5.2 | 23 |
| SYNS3-1800 | 650–1200 | 1800 | 20 | 5.2 | 25 |
| SYNS3-2000 | 800–1500 | 2000 | 15 | 6.8 | 28 |
| SYNS3-2400 | 1400–2000 | 2400 | 35 | 10.5 | 30 |
| SYNS3-2600 | 1400–2200 | 2600 | 50 | 13 | 38 |
| SYNS3-3000 | 2200–3200 | 3000 | 80 | 25 | 45 |
| SYC2-1300 | 50–200 | 350 | 8 | 0.4 | 2.5 |
Match the molding machine tonnage, mold opening and available headroom first. Then check payload including the gripper and workpiece, all three strokes, dry cycle time, mounting dimensions and air consumption. SYC2-1300 is for vertical thermoforming presses; other families serve horizontal injection molding machines.
EOAT selection guide ↗